Graphite Ore Beneficiation Process
The process of graphite ore beneficiation is relatively simple. Usually, three stages are required in the beneficiation process, namely crushing and screening, grinding and classification, and flotation.
Crushing and Screening: According to the large particle size of graphite ore, the first step in the process of graphite ore beneficiation is to grind the graphite ore. Graphite ore is crushed by vibrating feeder for the first process such as jaw crusher - coarse crushing, medium and fine crushing is carried out by cone crusher, and the graphite minerals obtained by fine crushing are screened. Usually a circular vibrating screen is used to screen out suitable ore for the next step of grinding and classification, and the graphite ore that does not meet the lumpiness during the crushing process is returned to be crushed again.
Grinding and Classification: The graphite ore obtained after crushing and screening is transported to a ball mill for grinding operation. After grinding, the graphite ore is subjected to classification treatment, and the qualified materials are sent to the next process.
Flotation: the graphite ore obtained after grinding is fully mixed with the flotation agent in the stirring tank, and the obtained graphite ore is put into the flotation machine for re-selection operation, and finally the graphite ore obtained by the flotation machine is dried, usually Use a dryer to obtain the final graphite concentrate powder.
]]>(1) Surface coating: a "protective film" is constructed to cover the graphite surface to form a "core-shell structure", which can avoid the peeling of graphite lamellae caused by solvation and improve the cycle stability of electrode materials. The coating of metal and its oxide can also reduce the resistance of lithium ion transfer and charge migration and improve the electrochemical performance of graphite materials.
(2) Chemical treatment: surface oxidation introduces oxygen-containing functional groups, increases the active site, forms a stable SEI film at the interface between anode material and electrolyte, and improves the cycle stability of carbon anode. Surface halogenation can form a passivation film with high intermolecular force on the surface of the material, which can improve the stability of the microcrystalline structure.
(3) Element doping: metal or non-metallic elements are incorporated into carbon anode materials to change the structure and electron arrangement of carbon microcrystals, so as to improve the electrochemical behavior of lithium ion removal and insertion in the anode materials.
The electrochemical performance of carbon anode materials can be greatly improved after surface modification, but the actual operation and regulation of each modification method will still affect the final modification effect. For example, the thickness of the coating layer, the degree of chemical treatment and the uniformity of heteroatom doping dosage, distribution and dispersion will affect the final performance of the material. If the control is not good, the performance of the lithium ion battery will not be improved, but the electrochemical performance will be degraded.
]]>At present, the commercial anode materials are mainly amorphous carbon (soft carbon and hard carbon), graphite (natural graphite and artificial graphite), lithium titanate and silicon based materials (silicon, silicon oxide and amorphous silicon), among which the graphite anode materials for power batteries account for more than 97% of shipments. However, the 360-365 mAh·g-1 capacity of high-end graphite products is close to the 372 mAh·g-1 theoretical gram capacity of graphite. The limited space to improve the energy density of batteries is hindering further improvement, so the development of high energy density of anode materials is the key to improve the cell energy density.
Silicon-based materials with a high specific capacity of 3579 mAh·g-1 and a low electrochemical lithium embedding potential of 0.4 V(vs.Li/Li +), as well as abundant resource reserves, are considered as the most potential anode materials for the next generation of high-energy density lithium ion batteries. Relevant studies have proved that the silicon negative electrode must be used when the cell energy density is greater than 280 Wh·kg-1 without the use of lithium rich anode. However, in the process of Li+ embedding, amorphous LixSi appears on the surface of silicon particles, while the internal silicon particles remain crystalline. When the degree of lithium increases to the full formation of Li22Si5, the theoretical capacity reaches the highest 4200 mAh·g-1, and the volume expansion is 320%, much higher than the 16% volume expansion of carbon material. The bulk deformation results in the destruction and repeated formation of the solid-phase electrolyte layer (SEI), resulting in the reduction of the first Coulomb efficiency (ICE) and the loss of active lithium ions. The low proportion of silicon anode materials mixed with graphite can increase the energy density and reduce the volume effect to a certain extent, but the low ICE problem still needs to be improved by corresponding technology.
Pre-lithiation technology is to add lithium source to the positive or negative electrode of the battery before battery activation to make up for irreversible capacity loss caused by SEI film in the process of initial battery cycle. Pre-lithiation technology is the most effective way to increase battery energy density, extend battery cycle life and improve battery ICE. At the same time, compared with the limited capacity of the positive electrode, the negative electrode prelithiation treatment can directly replenish lithium to the material and the unit mass of the material is large. Therefore, the negative electrode prelithiation technology is reviewed to provide a reference for improving the electrochemical performance of lithium ion batteries.
1.Lithium metal as a lithium source to supplement lithium
Lithium metal can be directly used as a lithium source for lithium pre-lithiation technology. Due to its low melting point (180 ℃), it is easy to be processed into lithium sheet, lithium belt, lithium particles and other forms under the condition of inert atmosphere or vacuum. At the same time, lithium metal itself is relatively soft and easy to be calendrated into film layer and attached. Therefore, the study of prelibiation using lithium metal as lithium source by different processes has attracted wide attention.
Lithium metal can be used directly in contact with the anode material or attached to the surface. Due to its low potential, lithium metal will be transformed into free Li+ in the electrolysis solution under the condition of electron exchange, and lithium embedding reaction will occur with the material. Kim et al. deposit lithium metal on the surface of the prepared silicon carbon electrode in the form of hot steam through vacuum heating deposition. At high temperature, the silicon-based material realizes lithium by directly contacting with lithium metal. At 0.1C ratio, the ICE of the full battery assembled by LiCoO2 positive electrode and pre-lithium Si-GR negative electrode increased from 76.4% to 92.5%, and the battery capacity increased from 138.2 mAh/g to 148.2 mAh/g. At the same time, the battery capacity retention rate was 80%. The number of cycles increased from 122 to 366 after pre-lithiation.
Rezqita et al. used lithium sheet as symmetric electrode and phenolic resin to prepare carbon silicon negative electrode assembly button battery under the action of external circuit, and obtained the carbon silicon material prelithium by electrochemical prelithium. The pre-lithiated silica and cathode Lini0.5Mn0.3Co0.2O2 can increase the ICE from 26% to 86%, while increasing the full battery capacity from 48 mAh/g to 160mAh/g. Yao et al. realized the pre-lithiation of silica by direct contact between lithium sheets and graphene-coated silica materials by short-circuit after the addition of electrolytic droplets. The graphene-coated silicon carbon material ICE was improved to 97.1% by short circuit prelithiation in direct contact with lithium metal for 5min. After 500 cycles of charge and discharge, the capacity of ICE was maintained at a current density of 969mAh/g at 2A/g, with good cycle stability.
The use of lithium metal can not only directly interact with the anode material, but also indirectly form the pre - lithium - replenishment effect on the anode material during the initial cycle of the battery. Stabilized lithium metal powder (SLMP) is a kind of negative electrode prelithium additive produced and developed by FMC company in the United States. Because of the inert protective layer Li2CO3 on its surface, it has good stability in the air. Pan et al. disperse SLMP in hexane in advance to form a uniform dispersion solution, and then spray on the surface of the prepared polar sheet to form a uniform SLMP layer. After the solvent volatilizes and rolls, the protective layer of SLMP breaks, making the negative silicon carbon material directly contact with lithium.
After the initial cycle, ICE increased from 68.1% to 98.5%, and the capacity retention rate was 95% after 200 cycles, showing good cycle stability. Due to the lithium has good ductility, Cao and so on through the metal lithium in the copper foil surface pressure into a thin layer of metal lithium layer, then as a protective layer in the surface with a polymer coating to protect metal lithium Damage will not be in the air oxidation, anode materials are then coated on top of the preparation of the active material / 3 layer structure of polymer/lithium metal electrode materials. The polymer layer will slowly dissolve in the electrolyte, eventually allowing the lithium metal to contact with the graphite material to complete the pre-lithiation and lithium replacement. In this way, a high ICE value of 99.7% was achieved for the graphite negative and even more than 100% ICE in the silicon nanoparticle negative.
The results show that lithium metal has a good role of supplementing lithium, which can improve ICE, energy density and cycle stability of batteries. However, lithium has strong activity to water and oxygen in the air, and the protection process is made into a complex lithium supplement process, which increases the cost to the actual production. The uniformity of the lithium replenishment process of pre-lithium needs to be further improved, and the formation of lithium dendrites after excessive lithium replenishment caused by uneven lithium replenishment is also a technological problem that needs to be solved.
2.metal lithium alloy compound as lithium source to supplement lithium
Due to its high activity, lithium metal is not conducive to electrode preparation. Similar to lithium metal, alloy complexes of lithium metal have low reduction potential and high capacity of lithium replenishment, which can be used as a substitute for lithium metal to realize lithium replenishment. However, the pure lithium alloy complex prepared by lithium metal, such as LixSi, has strong chemical activity, and will react quickly in the air exothermic reaction, so that direct use will still need complex protection engineering. Therefore, improving the chemical stability of lithium alloy is the key to make it become a rational prelibiation additive.
Zhao et al. prepared LixSi alloy by mechanical agitation of lithium metal and Si nanoparticles in accordance with a certain chemical and quantitative ratio, and then constructed Li2O oxide layer on the surface of LixSi with low oxygen content ratio in an inert atmosphere in the glove box. The core-shell LixSi-Li2O complex has certain stability in dry air, and LiXSi-Li2O can be used as a prelithium additive in polyvinylpyrrolidone electrode to increase ICE to more than 94%.
In order to further increase the stability of LixSi, Zhao et al. prepared LixSi/Li2O complex using low-cost SiO and SiO2. Due to the uniform distribution of Si and O atoms, the LixSi components are firmly embedded in the Li2O lattice generated from lithium, which makes them have good stability in the air with 40% humidity. Even if the structure of the surface LixSi collapses, the dense Li2O in the inner layer can still play a protective role. The low potential of the complex can achieve a good lithium replenishing effect on the anode material. As a pre-lithium additive, it can still provide a lithium replenishing capacity of 1 240 mAh/g after being exposed to the air for 6 h, and can still participate in the electrochemical cycle in the following cycle, showing a Coulomb efficiency of 99.87% in the 400 turn.
In addition to using silicon as the raw material for the preparation of lithium alloy compounds, Zhao et al. used the elements of the fourth main group (Z=Si, Ge, Sn) and the corresponding oxides to prepare alloy compounds Li22Z5 or Li22Z5-Li2O by one-step method. Li22Z5 or Li22Z5-Li2O alloy composites can play a good role of supplementing lithium for Sn base and graphite anode materials. According to chemical calculation, the binding energy of Ge and Li in LixGe is the highest compared with similar alloys, and it shows better stability in dry air. The dense Li2O lattice protection layer in LI22Z5-LI2O can greatly increase the stability of Li22Z5 in dry air, and the production process of direct mixing heating and stirring can reduce the cost of battery process improvement.
Compared with the high activity of lithium metal, the alloy compound LixZ of lithium has been greatly improved in stability, and some products can still maintain stability for 6 h in the air with 40% humidity. Moreover, the existence of Li2O lattice plays the role of skeleton support, so that the main active substance LixZ can still provide cycling capacity stably in the subsequent cycle process. However, the product can not be directly used in the water system sizing process of the negative mainstream, as a pre-libiation additive, because of its high activity. Therefore, it is of great practical significance to further improve the process of lithium alloy compound so that it can be directly used in water drainage slurry system.
3.molecular clips of lithium - aromatic compounds drive lithium supplementation
Molecular clipping compounds of lithium metal dissolved in organic solvents have been studied extensively. However, in different reducing organic solvents, for silicon-based materials with low potential, the lack of reduction of organic solvents will lead to insufficient addition of active lithium in silicon-based materials. At the same time, the method has the characteristics of good stability, high safety and mild reaction, so choosing appropriate reagents for prelithium is one of the effective methods to eliminate irreversible capacity loss.
Yan et al. used biphenyl (Bp) and gold lithium to construct LiBp reagent in tetrahydrofuran solution. SiOx/C was heated, stirred and filtered to obtain LIBP-SiOX /C complex in this reagent. After heat treatment, LIBP-SiOx /C is transformed into LixSiOy and evenly dispersed in SiOx/C, which can effectively inhibit the irreversible consumption of lithium ions. The material has high capacity and cycle stability. As a negative material, the soft coated battery prepared by matching LinI0.8Co0.1Mn0.1O2 positive material has a high energy density of 301Wh /kg and a capacity retention rate of 93.3% after 100 cycles. Wang et al. prepared LiBp prelithiation solvent by dissolving lithium gold, biphenyl and tetrahydrofuran solutions, and its low reduction potential of 0.41 V can effectively reduce the active substances.
At the same time, the LiBp reagent has strong stability in a certain humidity air atmosphere, can increase the ICE of phosphorus and carbon electrode material to 94%, has certain industrial use value. Shen et al. by using naphthalene lithium as the prelithium reagent to prepare the prelithium nano Si electrode, reducing the irreversible capacity loss of about 1 500 mAh/g, so that the first week efficiency of Si electrode improved to 96.1%. The prelithium electrode and the corresponding Si/Li2S-PAN electrode were used to assemble the full battery with the first efficiency of 93.1%, and the energy density was as high as 710 Wh/kg. Naphthalene lithium reagents are safer and cheaper than conventional lithium reagents, and the depth of lithium can be controlled by controlling the temperature and time.
Compared with the single study on naphthalene lithium reagent, Jang et al. made Li+ reduction potential in organic reagents controllable by selecting a series of biphenyl organic reagents and introducing different functional groups at different benzene ring positions. Low reduction potential is beneficial for Li+ to participate in the SEI formation of silica-based anode materials, and it can also directly act on the lithiation process of silica-based anode materials in the process of prelithiation. By controlling the immersion time of the electrode material in the organic reagent of the system, the ICE of the material can be increased to nearly 100%.
Studies have shown that the organic lithium reagents constructed by molecular shear of organic reagents can form a good lithium supplement effect on negative electrode materials, even low potential silicon-based materials. However, the organic reagent itself is expensive and has certain toxicity, which has a certain cost of technological transformation for the existing battery production. Therefore, it still needs further technological improvement in the face of large-scale use.
4. Conclusion and Prospect
The main material used in the anode of lithium ion battery is graphite. With the improvement of battery standards, the specific capacity and cycle life of the material need to be further improved. The pre-lithiation technology can further improve the overall energy density of the battery and reduce the loss of lithium ions during the first electrochemical cycle.
1) In metal lithium supplementing lithium, there are two ways to use metal lithium: direct contact and interjoint contact. The 3-layer electrode prepared by stabilized lithium metal powder and lithium foil calendering has been used commercially in bulk, but it has the disadvantages of uneven pre-lithiation and high cost. The lithium replenishment of metal lithium sheet involves the addition of control equipment of external circuit and the high time cost of lithium replenishment process, which is unfavorable to the demand of cost reduction in industrialization. Short circuit contact may face uneven lithiation phenomenon. Therefore, comprehensive advantages of various processes, the overall use of lithium metal in the lithium layer process still needs to be improved.
2) Lithium metal substitutes replace lithium with lithium alloy. Silicon lithium alloy compounds are added to the anode materials in the form of additives. However, due to their high activity, they are difficult to be stable in the air for a long time. However, for the direct use of water system slurry, the coating process still needs to be improved.
3) Lithium metal organic solvent, represented by lithium naphthalene reagent, has a low reduction potential and can play a good role in supplementing lithium to silicon-based materials with low potential. However, the actual lithium replenishment process involves equipment transformation and the increase of technological steps, which increases the difficulty of use to a certain extent. The expansion of application scope and the reduction of cost require further improvement of the process.
]]>Lithium iron phosphate battery belongs to lithium ion secondary battery, one of the main uses is for power battery, compared with Ni-MH, NI-CD battery has a great advantage.
The charging and discharging efficiency of lithium iron phosphate battery is higher than 90% in the case of rate discharge, while that of lead-acid battery is about 80%.
Safety Improvement
The P-O bond in lithium iron phosphate crystal is stable and difficult to decompose. Even at high temperature or overcharge, it will not collapse and heat or form strong oxidizing substances like lithium cobalt acid, so it has good safety. Some reports have pointed out that in the actual operation, a small number of samples were found to burn in the acupuncture or short-circuit experiments, but no explosion occurred. In the overcharging experiment, the explosion was still found when the high-voltage charging was much more than several times the self-discharge voltage. However, the overcharge safety of the battery is much improved compared with the ordinary liquid electrolyte lithium cobalt acid battery.
Improvement In Lifespan
Lithium iron phosphate battery refers to lithium ion battery which uses lithium iron phosphate as cathode material.
The cycle life of long life lead-acid battery is about 300 times, the highest is 500 times, while the cycle life of lithium iron phosphate battery is more than 2000 times, and the standard charge (5 hours rate) can reach 2000 times. Lead-acid batteries of the same quality are "new half a year, old half a year, maintenance and maintenance for another half a year", at most 1~1.5 years, and lithium iron phosphate batteries used under the same conditions, the theoretical life will reach 7~8 years. All in all, the performance price is more than four times that of lead-acid batteries in theory. High current discharge can high current 2C fast charge and discharge, under the special charger, 1.5C charge within 40 minutes can make the battery full, starting current up to 2C, and lead-acid battery has no such performance.
Good High Temperature Performance
The peak electric temperature of lithium iron phosphate can reach 350℃-500℃, while lithium manganate and lithium cobalt acid are only about 200℃. The operating temperature range is wide (-20C -- +75C), with high temperature resistance characteristics of lithium iron phosphate electric heating peak can reach 350℃-500℃, while lithium manganate and lithium cobalt acid only in about 200℃.
High Capacity
Has a larger capacity than ordinary batteries (lead acid, etc.). The monomer capacity is 5AH-1000AH.
No Memory Effect
When a rechargeable battery is constantly full, its capacity quickly falls below its rated capacity. This phenomenon is called memory effect. For example, nickel-metal hydride and nickel-cadmium batteries have memory, but lithium iron phosphate batteries do not have this phenomenon. No matter what state the battery is in, it can be used with charging, without first putting out and then charging.
Light Weight
The VOLUME of lithium iron phosphate battery with the same specification capacity is 2/3 of the volume of lead-acid battery, and the weight is 1/3 of lead-acid battery.
Environmental Protection
But some experts say that the environmental pollution caused by lead-acid batteries mainly occurs in the non-standard production process and recycling process of enterprises. Similarly, lithium batteries belong to the new energy industry is good, but it can not avoid the problem of heavy metal pollution. Lead, arsenic, cadmium, mercury, chromium, etc. may be released into dust and water during metal material processing. Battery itself is a kind of chemical substance, so it may produce two kinds of pollution: one is the pollution of process waste in the production engineering; Second, the battery pollution after scrapping.
Lithium iron phosphate battery also has its disadvantages: for example, the low temperature performance is poor, the positive electrode material vibration density is small, the volume of lithium iron phosphate battery with the same capacity is larger than lithium ion battery such as lithium cobalt acid, so it does not have advantages in the aspect of micro battery. When it comes to power batteries, lithium iron phosphate batteries, like other batteries, face the problem of battery consistency.
Power Battery Comparison
At present, the most promising cathode materials for power type lithium ion batteries mainly include modified lithium manganese (LiMn2O4), lithium iron phosphate (LiFePO4) and lithium nickel-cobalt manganese (Li(Ni,Co,Mn)O2) teramaterials. Nickel-cobalt lithium manganate ternary materials are generally considered to be difficult to become the mainstream of power lithium ion batteries for electric vehicles due to the lack of cobalt resources, the high price fluctuation of nickel and cobalt and other reasons, but can be mixed with spinel lithium manganate in a certain range.
Industry Application
Carbon coated aluminum foil brings technological innovation and industrial promotion for lithium industry; Improve the performance of lithium electric products and improve the discharge rate.
]]>1. The cathode material is mixed with metal foreign matter
When the anode material of iron (Fe), copper (Cu) and chromium (Cr), nickel (Ni), zinc (zinc), silver (Ag), and other metal impurity, battery into phase voltage after reaching the REDOX potential of metal elements, the metal will be first in the anode oxidation to the cathode reduction, when the cathode in metal elemental accumulated to a certain degree, The hard edges of the deposited metal Pierce the diaphragm, causing the battery to self-discharge. Self-discharge can cause fatal effects on lithium ion batteries, so it is particularly important to prevent the introduction of metal foreign bodies from the source.
There are many production processes of positive electrode materials, and every link in the manufacturing process will have the risk of introducing metal foreign bodies, which puts forward higher requirements for the equipment automation degree and on-site quality management level of material suppliers. However, due to cost constraints, material suppliers tend to have a low degree of equipment automation, more breakpoints in production and manufacturing processes, and an increase in uncontrollable risks. Therefore, in order to ensure stable battery performance and prevent self-discharge, battery manufacturers must promote material suppliers to prevent the introduction of metal foreign bodies from the five aspects of human, machine, material, method and ring.
First of all, from the personnel control, employees should not carry metal foreign matter into the workshop, do not wear jewelry, enter the workshop should wear work clothes, work shoes, wear gloves, avoid contact with metal foreign matter and then contact with powder. The supervision and inspection mechanism should be established to cultivate the quality consciousness of employees, so that they consciously comply with and maintain the workshop environment.
Production equipment is the main link of foreign body introduction, such as the equipment parts and tools in contact with the material rust, inherent material wear phenomenon; The equipment parts and tools that are not directly in contact with the material will float into the material due to the airflow in the workshop after dust adhesion. According to the degree of influence, different treatment methods can be adopted, such as painting, replacing with non-metallic material coating (plastic, ceramic), and wrapping bare metal parts. Managers should also formulate corresponding rules and regulations, make clear provisions on how to manage metal foreign bodies, develop a point inspection list, and require employees to check regularly to prevent problems.
Raw materials are the direct source of metal foreign matter in cathode materials. The content of metal foreign matter should be regulated for the purchased raw materials. After entering the factory, the content should be strictly inspected to ensure that the content is within the prescribed range. If the content of metal foreign matter in the raw material exceeds the standard, it is difficult to remove it in the subsequent process.
In order to remove the metal foreign bodies, electromagnetic iron process has become a production of the anode materials, electromagnetic iron removal machine is widely used, but the device of non-magnetic metals such as copper, zinc, etc, so the workshop should avoid the use of copper and zinc components, such as must be used also as far as possible don't direct contact with powder or bare in the air. In addition, the installation position, installation number and parameter Settings of the electromagnetic iron remover also have a certain impact on the iron removal effect.
In order to ensure the workshop environment, to achieve positive pressure in the workshop, the establishment of double doors, air shower doors to avoid dust from the outside into the workshop pollution material is also a very necessary measure, at the same time workshop equipment, steel structure should avoid rust, the ground should also be painted and regular magnetic removal.
2.The moisture content of the cathode material exceeds the standard
Most of the cathode materials are micron or nanometer particles, which are easy to absorb moisture in the air, especially the ternary materials with high N I content. When preparing the positive paste, if the water content of the positive material is high, the solubility of P V DF will be reduced after N M P absorbs water in the process of slurry stirring, leading to the jelly shape of the paste gel and affecting the processing performance. After the battery is made, its capacity, internal resistance, circulation and rate will be affected, so the moisture of the cathode material and the metal foreign matter should be as the key control items.
The higher the degree of automation of production line equipment, the shorter the exposure time of powder in the air, and the less water is introduced. Promote material suppliers to improve the degree of equipment automation, such as the realization of the whole pipeline transportation, monitoring the dew point of the pipeline, the installation of the manipulator to realize automatic charging and cutting contribute greatly to the prevention of moisture introduction. However, some material suppliers are limited by plant design or cost pressure, equipment automation is not high, manufacturing process breakpoints should strictly control the exposure time of powder, powder in the transfer process is best to use a nitrogen filled bucket.
Temperature and humidity in the production workshop is also a key control index. Theoretically, the lower the dew point, the better. Most material suppliers will focus on the moisture control after the sintering process. They believe that the sintering temperature of about 100 degrees can remove most of the moisture in the powder. As long as the moisture introduction from the sintering process to the packaging stage is strictly controlled, the moisture of the material can be guaranteed not to exceed the standard. Of course, this does not mean that there is no need to control the moisture before the sintering process, because if the moisture is introduced too much before the sintering process, the sintering efficiency and the microstructure of the material will be affected. In addition, the way of packaging is also very important, most material suppliers use aluminum bag vacuum packaging, it seems that this way is still the most cost-effective.
Of course, with different material designs, there will be great differences in water absorption, such as differences in coating materials and specific surface area, which will affect its water absorption. Some suppliers prevent the introduction of water in the manufacturing process, but the material itself is easy to absorb water, after the sheet is made of water is extremely difficult to dry out, which causes problems for battery manufacturers. Therefore, the problem of water absorption should be taken into account when developing new materials to develop materials with higher universality, which is of great benefit to both supply and demand.
3. The batch consistency of cathode material is poor
For battery manufacturers, the less different and more consistent the cathode material between batches, the more stable the finished battery performance. As we all know, one of the main disadvantages of lithium iron phosphate cathode materials is poor batch stability. In pulping, the viscosity and solid content of each batch of slurry are unstable due to large batch fluctuation, which brings trouble to users and requires constant adjustment of the process to adapt.
Improving the automation degree of production equipment is the main means to improve the batch stability of lithium iron phosphate material. However, at present, the equipment automation degree of domestic lithium iron phosphate material suppliers is generally low, the technical level and quality management ability is not high, and the materials provided have different degrees of batch instability. From the user's point of view, if the batch differences cannot be eliminated, we hope that the larger the weight of a batch, the better, provided of course that the same batch of materials are uniform and stable. Therefore, in order to meet this requirement, iron lithium material suppliers often add a step of mixing process after the finished product is made, that is, several batches of materials are evenly mixed. The larger the volume of the mixing kettle, the more materials are contained, and the larger the quantity of a batch is mixed. Lithium iron material particle size, specific surface area, such as moisture, pH indicators will affect the made into slurry viscosity, but often these indicators have strictly controlled within a certain range, but still there will be a batch of pulp viscosity differences, in order to prevent the abnormal, when batch use tend to simulate production formula preparation in advance before put into use some test paste viscosity, After meeting the requirements, the battery manufacturer will be put into use. However, if the battery manufacturer has to test before each production, the production efficiency will be greatly reduced. Therefore, the battery manufacturer will forward the work to the material supplier and require the material supplier to complete the test and meet the requirements before shipping. Of course, with the progress of technology and the improvement of process capacity of material suppliers, the distribution of physical property indicators is becoming smaller and smaller, so the step of viscosity testing before delivery can be eliminated. In addition to the measures mentioned above to improve consistency, we should use quality tools to minimize this batch instability and prevent quality problems.
]]>Update date: 2022/8/17
Effective Date: 2022/8/17
The Anode material production system is a product provided by Prominer(Shanghai)MiningTechnologyCo.,ltd (hereinafter referred to as "we"). When you use our services, we may collect and use your relevant information. We hope to explain to you through this "Privacy Policy" how we collect, use, store and share this information when using our services, and how we provide you with access, update, control and protection of this information. This "Privacy Policy" is closely related to the services of The Anode material production system you use. I hope you read it carefully and, when necessary, follow the guidelines of this "Privacy Policy" to make the choices you deem appropriate. For the relevant technical terms involved in this "Privacy Policy", we try to be concise and concise, and provide links to further explanations for your understanding.
By using or continuing to use our services, you agree to our collection, use, storage and sharing of your information in accordance with this Privacy Policy.
If you have any questions about this Privacy Policy or related matters, please contact us at [email protected].
Information we collect
The following information about you may be collected, stored and used by us or our third-party partners to provide services. If you do not provide relevant information, you may not be able to register as our user or enjoy some of the services we provide, or you may not be able to achieve the intended effect of the relevant services.
Personal information, the relevant personal information you provide to us when you register an account or use our services, such as phone number, email, etc.
Storage of Information
2.1 How and for how long the information is stored
We will store your information in a secure way, including local storage (such as data caching using APP), databases and server logs.
Under normal circumstances, we will only store your personal information for the time necessary to achieve the purpose of the service or under the conditions stipulated by laws and regulations.
2.2 Region of Information Storage
We will store user personal information collected in China in China in accordance with laws and regulations.
We do not currently transfer or store your personal information across borders. If cross-border transmission or storage is required in the future, we will inform you of the purpose, recipient, security guarantee measures and security risks of the information going abroad, and obtain your consent.
2.3 Notice when a product or service ceases to operate
When our products or services stop operating, we will notify you in the form of push notifications, announcements, etc., and delete your personal information or anonymize it within a reasonable period, unless otherwise provided by laws and regulations.
Information Security
We use a variety of security technologies and procedures to prevent loss, misuse, unauthorized access or disclosure of information. For example, in some services, we will use encryption technology (such as SSL) to protect the personal information you provide. However, please understand that due to technical limitations and various malicious means that may exist, in the Internet industry, even if we do our best to strengthen security measures, it is impossible to always guarantee 100% information security. You need to understand that the systems and communication networks you use to access our services may have problems due to factors beyond our control.
How we use information
We may use the information collected in the course of providing services to you for the following purposes:
to provide you with services;
For authentication, customer service, security, fraud detection, archival and backup purposes when we provide our services, to ensure the security of the products and services we provide to you;
help us design new services and improve our existing services;
Let us better understand how you access and use our services, so as to respond to your personalized needs, such as language settings, location settings, personalized help services and instructions, or to you and other users response;
Provide you with more relevant advertisements in lieu of generally-served advertisements;
To evaluate the effectiveness of advertising and other promotions and promotions on our Services and to improve them;
Software certification or management of software upgrades;
To allow you to participate in surveys about our products and services.
Information sharing
At present, we will not actively share or transfer your personal information to a third party. If there is other sharing or transfer of your personal information or you need us to share or transfer your personal information to a third party, we will directly or confirm The third party obtains your express consent to the above actions.
For the purpose of serving ads, evaluating and optimizing the effect of ad serving, we need to share some of your data with third-party partners such as advertisers and their agencies, and require them to strictly abide by our measures and requirements on data privacy protection, including but not It is limited to processing in accordance with the data protection agreement, letter of commitment and relevant data processing policies, to avoid identifying individuals and to ensure privacy and security.
We do not share information that can be used to personally identify you (such as your name or email address) with our partners unless you expressly authorize it.
We will not publicly disclose the collected personal information to the public. If it is necessary to publicly disclose it, we will inform you of the purpose of the public disclosure, the type of information disclosed and the sensitive information that may be involved, and obtain your express consent.
With the continuous development of our business, we may conduct mergers, acquisitions, asset transfers and other transactions, we will inform you of the relevant circumstances, continue to protect or require new The controller continues to protect your personal information.
In addition, according to relevant laws, regulations and national standards, we may share, transfer, and publicly disclose personal information without your prior authorization and consent in the following situations:
Those directly related to national security and national defense security;
Directly related to public safety, public health, and major public interests;
Those directly related to criminal investigation, prosecution, trial and execution of judgments;
In order to protect the life and property of the personal information subject or other individuals, but it is difficult to obtain the consent of the individual;
Personal information subjects disclose personal information to the public on their own;
Collect personal information from legally publicly disclosed information, such as legal news reports, government information disclosure and other channels.
Your rights
During your use of our services, we may provide you with corresponding operation settings depending on the specific situation of the product, so that you can inquire, delete, correct or withdraw your relevant personal information, you can refer to the corresponding specific guidelines to operate. In addition, we have set up a complaint reporting channel, and your comments will be dealt with in a timely manner. If you are unable to exercise your personal information subject rights through the above channels and methods, you can make your request through the contact information provided in this Privacy Policy, and we will provide feedback in accordance with laws and regulations.
When you decide to no longer use our products or services, you can apply for account cancellation. After canceling your account, we will delete or anonymize your personal information unless otherwise provided by laws and regulations.
Changes
We may amend the terms of this Privacy Policy from time to time. When changes occur, we will notify you of the new Privacy Policy when the version is updated, and explain the effective date to you. Please read the changed "Privacy Policy" carefully. If you continue to use our services, you agree that we will process your personal information in accordance with the updated "Privacy Policy".
Protection of minors
We encourage parents or guardians to instruct minors under the age of eighteen to use our services. We recommend that minors encourage their parents or guardians to read this Privacy Policy and advise minors to seek parental or guardian consent and guidance before submitting personal information.
]]>(1) Artificial graphite has become one of the main growth points. In the next few years, the new energy vehicle market will maintain a high growth trend under the support of the policy, artificial graphite will also be driven by the demand for power lithium, maintain a high growth rate, will become one of the main growth points of negative electrode materials in the future.
(2) Low-end repetitive capacity will be eliminated. Anode materials in the future enterprise product type switch to power market, a large part of the mainstream enterprise with the economies of scale and technological advantages, its market share will increase further, squeezed the market space, small business enterprise in the field of low-end positioning and the lack of core technology enterprises will face the risk on the acquisition or collapse.
(3) The industrialization process of silicon carbon negative electrode is accelerated. In the future, with the increase of energy density requirements of power batteries, the system of silicon carbon anode with high nickel ternary materials will become a development trend. In the next two years, with the technology of high-nickel ternary materials NCM811, NCA and other supporting materials gradually mature, the industrialization of silicon carbon anode is coming.
(4) The negative material is facing the pressure of cost reduction, and the natural graphite negative material has the competitive advantage of cost. With the decline of new energy vehicle subsidies, power lithium electric suppliers are facing pressure from downstream automakers to further reduce prices. Natural graphite anode materials will be more widely used in power lithium batteries of extended range electric vehicles due to the price advantage of raw materials and lithium iron phosphate anode materials. In addition, with the widespread application of energy storage in the scale of power system, lithium batteries with natural graphite anode materials and lithium iron phosphate anode materials will be more widely used due to their high cost performance advantages.
]]>2.Main furnace type and process of graphitization of anode material
At present, the furnace types used in the process of anode material graphitization mainly include Acheson graphitization furnace, internal series graphitization furnace, box type graphitization furnace and continuous type graphitization furnace, among which the most commonly used is Acheson graphitization furnace, and a small number of internal series graphitization furnace is used. Box-type graphitization furnace and continuous graphitization furnace are new furnace types developed in recent years. Box-type graphitization furnace develops rapidly, mainly through Atchison furnace renovation and partial new construction. Continuous graphitization furnace is newly built and still in the process of testing, its furnace type and process are not fully mature, and it will take some time for it to be widely used.
Atchison furnace is to install the carbon anode material in the single hole (1 hole crucible) crucible, and then the crucible is loaded into the graphitization furnace and the resistance material is installed between the resistance, and the two sides and the top cover are loaded into the insulation material to complete the graphitization through electricity transmission. The inner series graphitization furnace is to install the carbon anode material in the porous crucible (9 hole crucible), and then the crucible is connected end to end in the graphite furnace through the series connection mode, and the two sides and the upper cover are loaded with insulation materials to complete graphitization through electricity transmission. Box-type graphitization furnace is to load the carbon negative material directly into the large box installed with carbon plate or graphite plate in advance, and add carbon or graphite cover plate as the resistance, the upper and both sides of the heat preservation material into the graphitization through electricity transmission. Continuous graphitization furnace is to continuously add carbon anode material into the graphitization furnace chamber, after high temperature graphitization cooling discharge.
3.Key technical points in different graphitization furnace process
The processing of anode materials is mainly divided into two key links, granulation and graphitization, and both of them have high technical barriers. Anode materials through graphitization can significantly improve the specific capacity of anode materials, the first effect, specific surface area, compaction density, conductivity, chemical stability, such as performance index, so control and master good graphitization technology is an important approach to guarantee the quality of the anode materials, because of the box-type furnace and continuous graphitization furnace technology is not fully mature, The following focuses on the Atchison furnace and internal series graphitization furnace process points to do to introduce.
3.1 Loading of Acheson furnace and inner series furnace (crucible)
3.1.1 Volatiles collocation during furnace loading
When the temperature in the graphitization furnace rises to 200~1 000 ℃, a large number of volatiles will be discharged from the negative electrode in the furnace. If the volatiles cannot be discharged in time, it may lead to the accumulation of volatiles, which will cause the safety accident of the spraying furnace. When a large number of volatiles escape, volatiles combustion is not sufficient, will produce a large number of black smoke, resulting in environmental pollution or environmental accidents. Therefore, the following points should be paid attention to when loading the furnace:
(1) When installing the negative electrode furnace, it is necessary to carry out a reasonable collocation according to the volatile content level to avoid excessive concentration and concentration of high volatile parts in the process of power transmission;
(2) Appropriate air holes should be set on the top of the insulation material to play an effective escape;
(3) When designing the power supply curve, it is necessary to take full account of slowing down the curve appropriately in the concentrated discharge stage of volatiles, so that volatiles can be discharged slowly and fully burned;
(4) Reasonable selection of auxiliary materials, ensure the composition of auxiliary particle size, reduce the amount of 0~1 mm powder in the auxiliary materials, generally accounting for less than 10%.
3.1.2 Furnace resistance should be uniform when loading
When the negative electrode and resistance material are not evenly distributed in the furnace, the current will flow from the place with low resistance, and the phenomenon of bias current will occur, affecting the effect of graphitization of the whole furnace negative electrode. Therefore, the following points need to be paid attention to when loading the furnace:
(1) When loading the furnace, the resistance material should be discharged from the head of the furnace chamber to the tail long line of the furnace chamber to avoid concentration of small particles or large particles;
(2) the old and new crucible into the same furnace also need to be reasonable collocation, taboo new crucible with a layer, the old crucible with a layer of phenomenon;
(3) Avoid the resistance material exposed into the side wall material.
3.2 Acheson furnace and internal series furnace power supply
3.2.1 Basis for power curve formulation of anode material during power transmission
According to the different quality requirements of the cathode material, it can be divided into low temperature material (2 800 ℃), medium temperature material (2 950 ℃), high temperature material (3 000 ℃), but the graphitization high temperature treatment process is generally between 2 250 ℃ and 3 000 ℃, in order to make all positions in the furnace reach the required temperature, it is necessary to keep in the high temperature process for a period of time. In order to ensure the uniformity of temperature in the furnace, usually due to different furnace type, need to keep different time, general high temperature keep for 6~30 h, in the process of power transmission to prevent the furnace resistance rebound need to keep 3~6 h. The specific situation needs to be explored and formulated according to the following technical points.
(1) Select different heating curves according to the furnace core, anode material, resistance material, crucible, furnace loading amount, etc.;
(2) Different curves should be selected according to the volatiles of anode materials and resistance materials in the furnace. If the volatiles are high, a slower heating curve should be selected; otherwise, a faster one should be selected;
(3) When the ash content of the anode material and resistance material in the furnace is high or the anode material is relatively difficult to graphitization, the power transmission time should be appropriately extended.
3.2.2 Anode material power transmission process to prevent furnace injection accidents
Because the anode material is powdery material, volatile content is high and not easy to discharge, easy to produce arc and high volatile content caused by the furnace accident, the specific operation process should pay attention to the following matters:
(1) When the anode material is installed in acheson furnace, the resistance material should be ramped to avoid the arc caused by suspended resistance material between crucible during power transmission;
(2) the displacement change of the negative material of the inner series furnace is mainly reduced in the process of power transmission. Therefore, when the negative material is installed in the furnace, the stroke of the hydraulic cylinder should be calculated to ensure that there is a stroke and enough pressure in the process of power transmission, so as to avoid the arc spray furnace accident caused by the loss of pressure;
(3) Coarse particles and low volatile materials should be selected for both furnace types;
(4) In the process of power transmission, pay close attention to whether there is local heating in the furnace;
(5) In the process of power transmission, it is necessary to pay close attention to whether the furnace top and furnace wall have cross fire phenomenon;
(6) In the process of power transmission, it is necessary to pay close attention to whether there is a low roar in the furnace;
(7) It is necessary to pay close attention to whether there is a large fluctuation of current in the process of power transmission.
3.3 Cooling and baking
(1) In the process of graphitization cooling, the anode material can not be forced to cool by watering, but can be naturally cooled by grabbing the material layer by layer with grab bucket or suction device.
(2) Anode material crucible about 150 ℃ out of the best, early removal of crucible, due to high temperature, lead to anode material oxidation, specific surface area increases, will also lead to increased cost of crucible oxidation damage. Taking out the crucible too late will also make the cathode powder material oxidized, the specific surface area increases, the production cycle becomes longer and the cost increases.
(3) Under high temperature of graphitization at 3000 ℃, all elements except element C are vaporized and discharged. However, there will still be a small amount of impurities in the cooling process adsorption on the surface of the cathode, crucible surface will form a layer of rough hard shell, high ash, high volatile materials form more hard shell material. The selection of low ash and low volatile excipients is based on this reason.
(4) Hard shell material in the index and qualified anode material performance difference is great, so when taking out the crucible, it is necessary to knock off 1~5 mm thick hard shell material in advance for storage and storage separately, the qualified material with smooth surface is normally collected, put into the ton bag for storage and delivery to customers.
]]>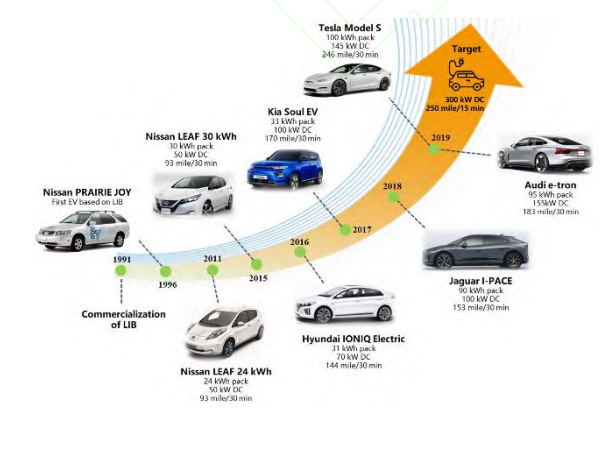
For the problems of graphite in fast charging, the current solutions are as follows.
(1) Constructing a stable artificial SEI membrane. By constructing an organic/inorganic artificial SEI film with stable structure, high redox potential and good ionic conductivity on the graphite surface, it can not only reduce the anisotropy of lithium ion transport in graphite, but also improve the migration rate of lithium ions. Small polarization to avoid the deposition of lithium metal on the graphite surface during high-rate charge and discharge. In addition, the artificial SEI film can also serve as a "differentiating sieve" for lithium ions and solvent molecules, avoiding the damage of the graphite structure caused by the co-intercalation of solvent molecules.
(2) Morphology and structural design. By modifying the morphology and structure of graphite (such as hole structure design), the number of active sites for edge intercalation of graphite can be increased, and the mobility of lithium ions in graphite can be improved.
(3) Electrolyte optimization. By optimizing the use of solvents, regulating the type and concentration of lithium salts, and adding organic/inorganic additives, the solvation structure of lithium ions in the electrolyte can be effectively adjusted, the desolvation barrier of lithium ions can be reduced, and a stable SEI film can be constructed. As well as mitigating the effect of solvent molecular co-intercalation on graphite stability.
(4) Optimize the charging strategy. By optimizing the charging protocol, regulating the charging current, voltage and relaxation time, the charging rate limit can be reached without the formation of lithium dendrites, and the balance between cycle life and charging rate can be achieved. These methods can effectively improve the capacity and stability of graphite under fast charging conditions, and provide a reference for the realization of "refueling" charging of electric vehicles.
However, the fast charging design of graphite still has the following challenges:
(1) The chemical stability of graphite is extremely strong, and the wettability of the surface is very poor. Therefore, it is difficult to construct artificial SEI protective films by some simple physical and chemical methods. Most of the current research needs to use ALD atomic layer deposition, CVD vapor deposition and other methods. These methods to construct artificial SEI protective films have high cost, cumbersome process, low efficiency, and do not have the feasibility of large-scale industrialization. Therefore, how to start with graphite itself and change its intrinsic physical and chemical properties, so as to realize the construction of artificial SEI protective film in a simple and convenient way, is the focus of future research.
(2) By designing pores and reducing the morphology and structure of graphite particles, although the lithium intercalation sites of graphite can be increased, the increase of active sites is often accompanied by the intensification of side reactions and the decrease of the first Coulombic efficiency. Given that the price of lithium salts has reached an all-time high, the fast-charging design of graphite cannot come at the expense of increasing the irreversible capacity for the first time. Therefore, the regulation strategy of morphology and structure must be used in conjunction with other surface modification strategies to avoid additional lithium consumption.
(3) By using functional additives or developing new lithium salts and solvents, it is crucial to obtain novel electrolytes with high ionic conductivity, high transfer numbers, and wide temperature ranges, as electrolytes determine ion transport and interfaces for specific battery chemistries. However, the development guidelines of electrolytes must take into account the cost factor and environmental protection degree, otherwise it will lack practical significance.
(4) Most of the graphite-based fast charging designs are still evaluated based on button batteries. As a technology that urgently needs large-scale industrial application, researchers should evaluate it in pouch cells or cylindrical cells to verify its commercial application potential.
]]>At present, various anode and anode materials and corresponding electrolytes have been developed and applied in lithium ion batteries. The cathode material widely used in commercial batteries is graphite, mainly including meso-phase carbon microspheres (MCMB), artificial graphite and natural graphite. Lithium ion batteries made of graphite are mainly used in portable electronic products. Modified graphite has been used in power batteries and energy storage batteries. The specific capacity of high-end graphite products on the market is close to the theoretical value of 360mA• H •g−1, and has excellent cycling performance, which is difficult to further improve. Simulation results show that increasing the specific capacity of the cathode material within 1200mA•h•g−1 is still a great contribution to improving the energy density of the battery.
At present, the main problem in the preparation of Si/ graphite composites is how to ensure the uniform and stable composite of nano-Si and graphite, so that the composites can take into account both high specific capacity and cyclic stability. In general, the preparation of Si/ graphite composites with nano-Si and graphite as raw materials needs to be combined with a variety of technical means. In this paper, we only use the one-step technique of Si and graphite combination to classify, mainly including solid-phase mixing method, liquid phase process and vapor deposition process.
2.1 Solid-phase Mixing Method
In the early stage, researchers mainly prepared Si/ graphite composites by simple mechanical mixing, namely solid phase mixing method. Although the solid-phase recombination method is simple, the combination of Si and graphite is not close, and a large amount of Si is exposed in the electrolyte, which has an adverse effect on the electrochemical performance.
For example,Cheng et al. used a high-energy mechanical ball mill to grind micron Si powder, graphite powder and multi-walled carbon nanotubes in a stainless steel ball mill tank to obtain a mixture of nano-Si/graphite/multi-walled carbon nanotubes, in which the Si content is 33wt%. Electrochemical tests showed that the first reversible specific capacity was about 2000mA•h•g−1 when the current density was 35mA•g−1, and the reversible specific capacity remained at 584mA•h•g−1 after 20 cycles.
Xu et al. prepared Si nanowire with a diameter of about 100nm by metal catalytic etching, and then directly ball-milling 15wt% Si nanowire with micron graphite powder to prepare Si nanowire/graphite anode material. The first Coulomb efficiency was 74% and the reversible specific capacity was 514mA after 15 cycles • H • G −1.Yin obtained Si/Mn/ graphite micron-grade composites by mechanical ball milling of micron-grade Si powder, Mn powder and graphite, in which the Si content was 20wt%. The first coulomb efficiency is 70%, and the reversible specific capacity is 463mA•h•g−1 after 20 cycles, when the current density is 0.15mA•cm−2.
Whittingham et al. obtained Si-Al-graphite composites by mechanical ball milling of Si powder, aluminum powder and graphite, with Si content of 7.9%. At 0.5mA•cm−2 current density, the first reversible specific capacity is 800mA•h•g−1 and the coulomb efficiency is 80%. After 10 cycles, the reversible specific capacity remains about 700mA•h•g−1.
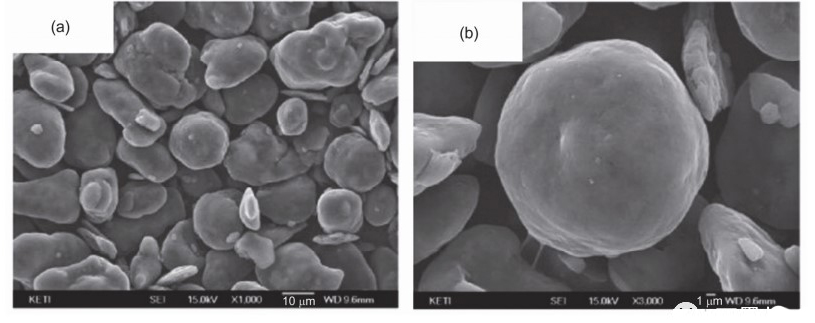
Kim et al. prepared nano-Si powder by ball milling micron Si powder and then compounded it with pitch and graphite sheet. After mechanical granulation and high temperature calcination, nano-Si/amorphous carbon/graphite spherical composite material was obtained, in which Si content was about 20%. The structure of the product is shown in Figure 2. Electrochemical tests show that the first reversible specific capacity is 560mA•h•g−1 at the current density of 140mA•g−1, the first coulomb efficiency is 86%, and the reversible specific capacity remains 80% after 30 cycles. The introduction of the third phase M(M = metal, graphene or amorphous carbon) can promote the close bonding between Si and graphite, and is conducive to increasing the electrical conductivity of the material, which provides a new design idea for the preparation of Si/ graphite composites.
2.2 Liquid phase complex method
The liquid phase composite process can make the raw materials disperse more evenly in a mild environment, and usually introduce the third phase substance M(amorphous carbon, graphene, metal, metal silicide, etc.) to promote the combination of Si and graphite, which is the main direction of Si/ graphite composites preparation.
Guo et al. fully dispersed nano-Si, citric acid and flake graphite in ethanol solution. After drying, they calcined at 500℃ to obtain nano-Si/amorphous carbon/graphite composites, in which amorphous carbon tightly "bonded" nano-Si to the surface of graphite, and the mass fraction of Si was about 7.2%. Electrochemical tests show that the first coulomb efficiency is about 80% and the reversible specific capacity is 476mA•h•g−1 when the current density is 0.1A•g−1, and the specific capacity remains 86% after 100 cycles.
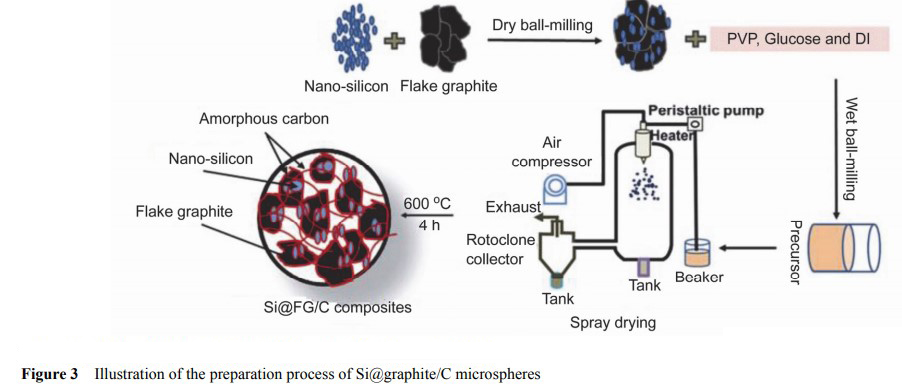
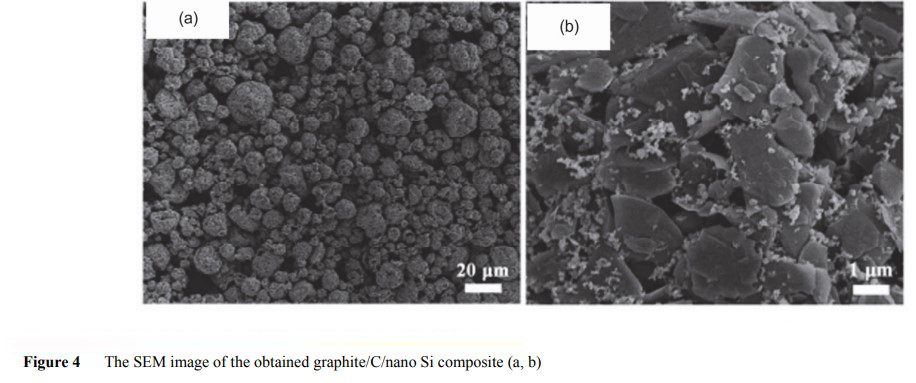
Cao et al. used commercial nano-Si powder and graphite sheet as raw materials, combined with mechanical ball milling, spray drying technology and high temperature calcination to obtain nano-Si/amorphous carbon/graphite composites, in which Si content is about 10%. Figure 3 shows a flow chart of the preparation process. The final samples obtained are micron particles composed of graphite sheets, Si nanoparticles and amorphous carbon, as shown in FIG. 4. Under the current density of 0.2A•g−1, the coulomb efficiency of the first ring is 74%, and the reversible specific capacity is 587mA•h•g−1. The reversible specific capacity is maintained at 420mA•h•g−1 for 300 cycles at A current density of 0.5A•g−1.
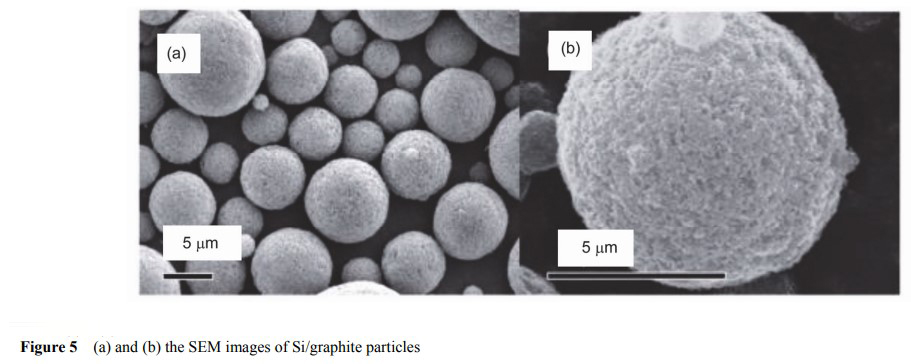
Su, such as using mechanical ball grinding micron size Si powder preparation of nanometer Si powder (100 nm), in water solution, the nano Si, glucose, graphitized carbon nano ball evenly dispersed, after spray drying granulation into micro ball precursor, after 900 ℃ calcination process in inert gas for Si/amorphous carbon/graphite composite materials, including Si content is 5 w t%. The resulting product is a micron sphere with multistage structure, as shown in Figure 5. Electrochemical measurements show that the reversible specific capacities are 435 and 380mA•h•g−1 at 500 and 1000mA•g−1, respectively. After 100 cycles of 50mA•g−1, the reversible specific capacity is 483mA•h•g−1, but the first coulomb efficiency is only 51%, mainly because nano-sized particles have large specific surfaces and form a large number of SEI films.
Kim et al. first dissolved coal pitch in tetrahydrofuran, and then added nano-Si powder and graphite microspheres. After ultrasonic dispersion, tetrahydrofuran is evaporated to obtain a precursor mixture, in which the ratio of Si to graphite can be controlled by adding raw materials. After calcination at 1000℃ in Ar atmosphere, amorphous carbon generated from asphalt pyrolysis "sticks" Si nanoparticles closely to the surface of graphite microspheres, as shown in FIG. 6. The final product is "potato shaped" particles, and Si nanoparticles are uniformly compound in the outer layer of graphite spheres.
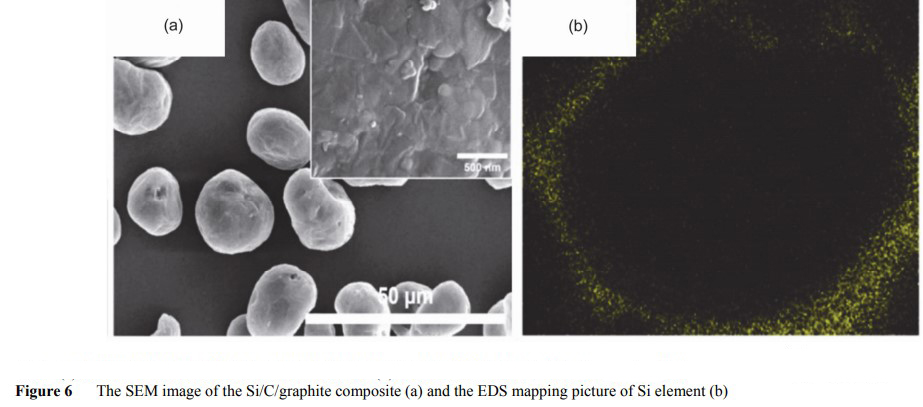
When the current density is 0.15A•g−1, the first reversible specific capacity and the first coulomb efficiency of the composites with Si mass fraction of 15% are 712mA•h•g−1 and 85% respectively. After 100 cycles, the reversible specific capacity remains 80%. With the increase of Si content, the specific capacity of the composite is improved, but the cyclic stability is not so high, mainly due to the volume expansion of Si.
2.3 Chemical vapor deposition
Chemical vapor deposition is mainly based on graphite. Si is deposited on graphite surface by pyrolysis of silane at high temperature. The biggest advantage of vapor deposition is that Si nanoparticles can be uniformly distributed on the surface of graphite. Holzapfel et al. directly grew a layer of Si nanoparticles on the surface of graphite sheet by chemical vapor deposition (Si particle size is 10-20nm, mass fraction is 7.1%). Electrochemical tests show that the first reversible specific capacity is 520mA•h•g−1, coulomb efficiency is 75%, and the reversible specific capacity is 470mA•h•g−1 when the current density is 10mA•g−1.
Cho et al. obtained porous graphite by etching graphite microspheres catalyzed by metal nickel, and then grew Si nanowires on porous graphite by catalytic cracking silane of metal gold. Si nanowires/graphite composites were obtained with the mass fraction of Si being 20%. Figure 7 shows the simulation diagram of the preparation process. When the current density was 0.05c (1C = 1050mA•h•cm−2), the reversible specific capacity and coulomb efficiency of the first cycle were 1230mA•h•cm−2 and 91%, respectively. The reversible specific capacity was 1014mA•h•cm−2 for 100 cycles at 0.2c, and no obvious attenuation was observed.
3 Summary and Prospect
In summary, the composite process of Si nanocrystalline graphite mainly includes solid phase method, liquid phase method and gas phase deposition method, combined with spray drying, mechanical granulation, high temperature sintering and other technical means. In general, the introduction of a third phase material (amorphous carbon, graphene, metal, metal silicide) can further promote the uniform recombination of Si and graphite, so that the two are tightly "bonded" together, while forming a three-dimensional conductive network and avoiding direct contact between the nano Si and the electrolyte.
]]>